Every minute your boil kettle runs, it releases boiling-hot secondary steam — brewers call it vapor. Did you know that turning just 1 kg of 100 °C water into 100 °C steam costs roughly 2,260 kJ of heat energy? And that every cubic meter of vapor you vent not only throws that energy away, but also carries malt and hop aromas your neighbors will complain about? Breweries that recover this heat can cut boiling energy consumption by up to 64%. So how do the three proven recovery systems actually work — and which one fits your brewhouse?
Why does vapor from the boil kettle carry so much energy?
During a 90-minute boil, a typical brewhouse evaporates 8–12% of the wort volume. All of that evaporated water leaves the kettle as saturated vapor at about 100 °C, and every kilogram of it carries roughly 2,260 kJ of latent heat. Vent it straight up the stack and two problems hit you at once:
- Energy is lost. A 50 hL batch with 10% evaporation releases about 500 kg of vapor — more than 1,100,000 kJ of recoverable heat per brew, batch after batch.
- Odor pollution builds. Vapor carries volatile malt, hop and DMS-related aroma compounds into the neighborhood — an increasingly common regulatory headache for city breweries.
How can this heat be captured instead? The brewing industry relies on three battle-tested approaches: the vapor condenser, vapor compression, and low-pressure boiling with thermal energy storage. Let’s walk through each one.
How does a vapor condenser turn waste steam into useful hot water?
The vapor condenser is the simplest and most widely used heat-recovery technology in the industry: modest investment, easy retrofit, fast payback. It is installed at the vapor stack outlet of the boil kettle, where rising vapor flows through a shell-and-tube heat exchanger and transfers its heat to water.
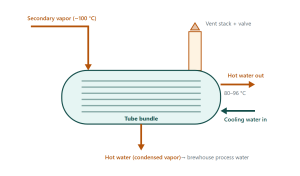
The numbers speak for themselves. For every 100 L of wort boiled, the condenser typically delivers around 80 L of 80 °C hot water. The outlet temperature depends on how you boil:
- Atmospheric boiling: outlet water temperatures up to 96 °C.
- Low-pressure boiling: hotter vapor means water up to 102 °C.
Where does all this hot water go? Straight back into the process. It serves as mashing-in water or sparging water in the lauter tun, displacing large amounts of primary steam that would otherwise be burned to heat cold brewing liquor. And because the vapor itself condenses into hot water, nothing is left to waste.
One-stage or two-stage condensation?
Depending on the intended use, vapor condensation can run as a one-stage or two-stage system. Two-stage design heats water to a high temperature in the first stage, then uses the leftover low-grade heat in the second stage to warm cold water — extracting the maximum possible heat from every cubic meter of vapor.
In practice, though, a brewery running several batches per day produces more hot water than the brewhouse can absorb. Hot water only equals saved energy if someone actually uses it. That is why most breweries deliberately pick the simpler one-stage condenser — matching recovery to their real hot-water balance rather than chasing theoretical maximum efficiency.
Rule of thumb: a condenser is only as valuable as the hot-water demand behind it. Before investing, map your daily consumption — mashing-in, sparging, CIP, cleaning — and size the condenser to match.
Vapor compression: can you boil wort with the steam you already have?
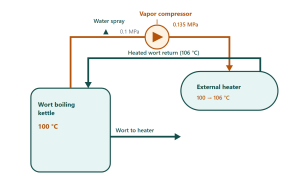
Condensing vapor into hot water recovers heat — but what if you could reuse the vapor as heating steam directly? That is exactly what a vapor compression system does. A compressor takes the kettle’s own vapor (about 0.1 MPa) and squeezes it to 0.135 MPa of superheated steam. Compression raises the steam temperature above 100 °C, so it can condense against boiling wort and hand its latent heat back to the very same kettle — a beautifully closed loop.
Vapor compression with an external boiler (external wort boiling)
Most vapor compression installations use an external wort heater, because the heat-transfer surface must be very large to condense the compressed steam efficiently. Wort circulates rapidly between the kettle and the external heater, where the compressed vapor delivers its energy.
Vapor compression with an internal heater
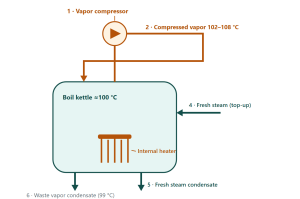
An internal-boiling kettle can carry a vapor compressor too. Here, the compressed vapor (102–108 °C) is fed directly into the kettle’s internal heater, where it condenses and drives the wort fountain.
What are the real advantages — and the catches?
The benefits are compelling:
- Large savings in primary steam — the kettle largely heats itself with its own vapor.
- No surplus hot water to dispose of, unlike a condenser installation.
- No odor emissions and no environmental pollution from vented vapor.
- Easy retrofit — the compressor can be added to existing wort boiling equipment, which is why it appeals to breweries that don’t want to switch to low-pressure boiling.
But be honest about the challenges too:
- The compressor consumes a significant amount of electricity — the economics depend on your local steam-to-power price ratio.
- No air may enter the compression system. Air is incondensable; even small leaks dramatically reduce heat transfer and system performance. The kettle must run at a slight vacuum of about 0.003 MPa below atmospheric, so vessels and seals face stricter demands, along with extra maintenance and monitoring.
- Startup energy is required. Because the system runs on low pressure, a jet pump fed with roughly 1 MPa of high-pressure primary steam is used at start-up to draw vapor out of the boil kettle and get heating going.
Low-pressure boiling with thermal energy storage: the game-changer?
Here is a paradox every brewer recognizes: the brewhouse produces enormous quantities of low-grade hot water — far more than it needs — while simultaneously burning primary steam to make the high-grade hot water that mashing and boiling actually demand. Low-grade heat cannot meet process temperatures, so it is dumped, and energy is wasted twice.
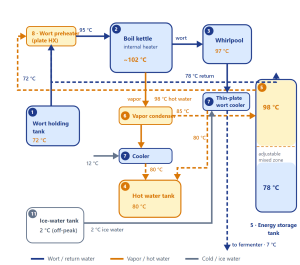
The low-pressure boiling system with energy storage resolves this elegantly. Its heart is a tall, stratified energy storage tank — typically 10–20 m high — in which 98 °C high-grade water floats on top of 78 °C low-grade water, separated by an adjustable mixed zone. The interface height can be tuned to the day’s production plan, and the thermal battery keeps surplus heat stored for long periods, ready for reuse at any time.
How does the energy flow through the system?
Follow the heat, step by step:
- Vapor condensation (charging the battery). Vapor from the boil kettle (2) enters the vapor condenser (6) and is cooled to 85 °C. This vapor heat warms the 78 °C water in the lower half of the energy storage tank (5) up to 98 °C, which then flows into the tank’s upper half.
- Cold-water preheating (harvesting the leftovers). The 85 °C water leaving the condenser is cooled further — down to 30 °C — in the condensate cooler (7), and in doing so heats 12 °C cold water up to 80 °C for the hot water tank (4).
- Wort preheating (discharging the battery). Wort held in the storage tank (1) at about 72 °C is heated in the plate heat exchanger (8) by 98 °C water from the tank’s upper half to 95 °C before entering the kettle — slashing the kettle’s own heating workload. The 98 °C water leaves the exchanger cooled to 78 °C and returns to the lower half of the tank.
- Wort cooling with ice water (the second recovery loop). Clear wort at 95 °C leaves the whirlpool (3) and enters a one-stage thin-plate cooler (7), where 2 °C ice water brings it to pitching temperature (about 7 °C). The ice water warms to 80 °C along the way and flows into the hot water tank (4). The 2 °C ice water itself is made during off-peak, low-tariff hours and parked in a well-insulated ice-water tank — another quiet cost saver.
Why does tank height matter so much?
Stratification is physics doing free work: hot water is less dense and floats, cold water sinks, and the boundary between them — the mixed zone — is the system’s “state of charge”. The taller the tank, the more precisely the 98 °C/78 °C interface can be positioned to match production. That is why these storage tanks are built 10 to 20 m tall, and why the mixed-zone height is treated as an adjustable operating parameter rather than a fixed property.
How much energy does wort boiling actually consume?
In wort production, the boil kettle is the single largest steam consumer — so any serious energy-saving program starts there. Consumption is expressed in kW·h or kJ (1 kW·h = 3,600 kJ). Comparing common fuels makes the stakes concrete:
Table 1. Calorific values of common industrial fuels
| Fuel |
Calorific value |
| Natural gas |
11.2 kW·h/m³ |
| Fuel oil |
10.14 kW·h/L |
| Heavy oil |
11.16 kW·h/kg |
| Coal |
8.95 kW·h/kg |
Now compare the boiling systems themselves. A traditional boil at 100 °C for 90 minutes with 12% total evaporation needs about 14 kW·h (50,400 kJ) per 100 L of cast wort. Low-pressure boiling shortens the boil to 60–70 minutes and trims evaporation from 12% (10–15%) to 5–7%, cutting consumption to roughly 9 kW·h per 100 L. And a brewhouse with an energy storage system gets down to approximately 5 kW·h (18,000 kJ) per 100 L — a 64% saving against the traditional benchmark:
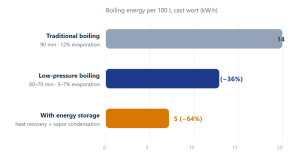
The energy-storage route deserves a closer look. In this configuration, the 78 °C water from the lower half of the storage tank is heated to 96 °C by kettle vapor in the condenser, then parked in the tank’s upper half. The vapor’s heat is thus stored as high-grade hot water and used as the mashing-in water for the next batch — cutting the brewhouse’s hot-water demand at the source. Measured against conventional boiling without recovery (at 5% evaporation), the energy-storage system saves about 9 kW·h per hectoliter of cast wort, leaving a net heat consumption of only about 5 kW·h per 100 L.
What could these savings be worth every year?
Translate the engineering into money. At roughly 9 kW·h saved per hectoliter, annual heat recovery scales directly with production volume — and the numbers get serious fast:
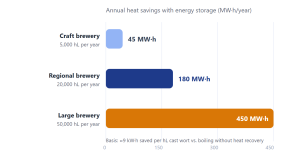
And that is only the fuel side. Add the hot water the system delivers (which displaces heated brewing liquor), the avoided odor-abatement equipment, and the carbon footprint reduction that more and more markets now price in — and the payback conversation changes completely. For a mid-size regional brewery, the question is rarely whether the system pays for itself; it is how many years you want to keep paying the alternative.
Which energy-saving system fits your brewery best?
Each of the three technologies answers a different question — so the right choice depends on your priorities, existing equipment and utility prices:
Table 2. Comparison of wort boiling energy-saving systems
| Système |
Investment & complexity |
Main benefit |
Watch out for |
Best suited for |
| Vapor condenser |
Low investment, simple technology |
~80 L of 80–96 °C hot water per 100 L wort boiled; fast payback |
Hot-water surplus if brewhouse demand is small |
Most breweries; the default first step |
| Vapor compression |
Medium–high; compressor + tight air-sealing, extra maintenance |
Reuses vapor as heating steam directly; no surplus hot water; no odor emissions |
Electricity consumption; strict vacuum (0.003 MPa) and sealing; jet-pump startup steam |
Breweries retrofitting existing kettles that don’t want low-pressure boiling |
| Low-pressure boiling + energy storage |
Highest; tall stratified tank (10–20 m) plus condenser and exchangers |
Up to 9 kW·h saved per hL; heat stored for reuse anytime; shorter boil (60–70 min) |
Space for the tall tank; more sophisticated controls |
New brewhouses and multi-brew days with large hot-water swings |
What mistakes should you avoid when investing in heat recovery?
Learn from the projects that disappointed:
- Sizing recovery to theory instead of demand. A condenser that makes more hot water than your brewhouse can use is a radiator, not an investment. Start from your measured hot-water balance.
- Ignoring air leaks. Vapor compression lives or dies by airtightness — inspect gaskets, valve stems and seals before blaming the compressor.
- Skipping insulation on storage. A stratified tank loses its value if the 98 °C layer bleeds heat into the brewhouse roof. Insulate the shell and every penetration.
- Missing the tariff arbitrage. Ice-water generation and hot-water storage can be shifted into off-peak hours — thermal storage without load-shifting leaves money on the table.
Frequently asked questions about wort boiling energy savings
How much hot water does a vapor condenser really produce?
As a rule of thumb, every 100 L of wort boiled yields about 80 L of 80 °C hot water. With atmospheric boiling the outlet can reach 96 °C, and with low-pressure boiling up to 102 °C — hot enough for mashing-in and sparging without further heating.
Why do most breweries choose one-stage condensation over the more efficient two-stage design?
Because multi-brew days generate more hot water than the brewhouse can use. Two-stage extraction maximizes heat recovery, but unrecovered hot water is wasted value. One-stage systems match production reality and cost less — so they dominate in practice.
Can a vapor compressor be retrofitted to an existing boil kettle?
Yes. Vapor compression systems can be installed on existing wort boiling equipment, which is precisely why they appeal to breweries that don’t want to switch to low-pressure boiling. The main requirements are a large heat-transfer surface (usually an external heater) and an absolutely airtight vapor circuit.
Why must no air enter a vapor compression system?
Air is incondensable. It accumulates on the condensing surface and acts as an insulation layer, sharply reducing heat transfer and system performance. That is why the kettle operates at a slight vacuum (~0.003 MPa) and why sealing quality is a top maintenance priority.
How long does it take for a vapor condenser to pay for itself?
It depends on your fuel price and hot-water demand, but because the condenser is the cheapest of the three systems and works on every single brew, payback is typically measured in months to a couple of years for breweries with a solid hot-water balance.
How tall is a stratified energy storage tank, and why?
Typically 10–20 m. Height creates stable thermal stratification: 98 °C water floats above 78 °C water with a thin, adjustable mixed zone. The interface height acts as the “state of charge” and can be tuned to the brewery’s production schedule.
What is the single biggest energy consumer in wort production?
The boil kettle. Traditional 90-minute boiling with 12% evaporation needs about 14 kW·h per 100 L of cast wort — which is exactly why every serious energy-saving program starts with the boiling system.
Conclusion: stop venting profit into the sky
Every kilogram of vapor carries about 2,260 kJ of heat, and a traditional boil releases hundreds of kilograms of it per batch. Whether you start with a simple vapor condenser, retrofit a vapor compressor, or design a low-pressure boiling system with thermal energy storage from day one, the physics works in your favor: the same heat that boils your wort can mash your next batch, sparge your lauter tun, and warm your brewing liquor — almost for free. Cut boiling energy by up to 64%, shrink your carbon footprint, silence the odor complaints, and let thermal stratification work the night shift at off-peak tariffs. In modern brewing, the question is no longer whether to recover boiling heat — but how quickly you can start.


 Publié