Brewhouse Calculations: How Much Malt, Water and Mash Do You Really Need per Brew?
Brewhouse Calculations: How Much Malt, Water and Mash Do You Really Need per Brew?
نُشر
بقلم زيرين
How much malt goes into 150 hL of 12 °P wort? How much water should the mash carry? And how much mash must you pull to boil in a decoction brew? Behind every consistent brewhouse sits a handful of plain formulas — grist bills, mixed extract, mashing water, decoction volumes and raw-material utilization. Work them once, and you will never guess a charge weight again.
What goes into the grist bill — and in what ratio?
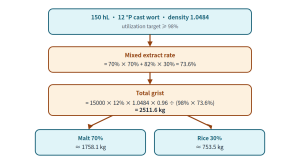
Adjunct brewing starts with a ratio. Common grain bills run 70% malt / 30% rice, 75% malt / 25% rice, or 65% malt / 35% rice. Once the ratio is fixed, three questions follow: what extract can the blend deliver, how much blend does the brew need, and how does that split back into malt and adjunct?
How do you blend malt and adjunct extract potentials?
The laboratory supplies a theoretical extract for each raw material. The blend’s extract is simply the weighted average:
Total grist follows from the wort output, its gravity, and one small correction — the 0.96 volume-shrinkage factor (wort contracts by about 4% when it cools from 100 °C to 20 °C):
One practical caveat: laboratories quote extract on a dry or air-dry basis, while the brewhouse buys, mills and mashes a slightly wetter material — so actual charges often land a little above the calculated figure. Keep the formula as your baseline and reconcile it against your own utilization trend.
How much water does the mash actually need?
Brewers express mashing water as a water-to-grist ratio — litres of water per 100 kg of raw material. But there is a second way in: fix the first-wort concentration you want, and let the formula tell you the water. If only malt is used (no cereal adjuncts), let its extract rate be W % — i.e. 100 kg of malt carries W kg of soluble material — and let the first-wort concentration be Wp (°P) for a 100 kg charge with V litres of mashing water. The mass-balance law of averaging gives:
Wp = 100W ÷ (W + V) → V = W(100 − Wp) ÷ Wp
Worked example 2 — 16 °P first wort from 72% extract malt
V = 72 × (100 − 16) ÷ 16 = 378 L of water per 100 kg of malt
If cereal adjuncts are in the grist, first compute the mixed extract rate (exactly as in the grist-bill section), then feed that blended W into the same formula for the total mashing water.
Decoction mashing — how much mash must you pull to boil?
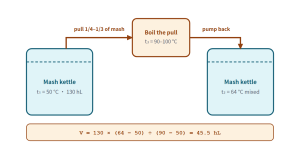
In a decoction program, part of the mash is pumped out, boiled, and returned to the remaining mash to lift it to the next rest temperature. How big is the pull? Experience says the boiled fraction is about one quarter to one third of the total mash. For the exact figure, use a heat balance:
V = V₁(t₂ − t₁) ÷ (t₃ − t₁)
where V = mash volume to pull (hL), V₁ = total mash after mixing (hL), t₁ = mash temperature before the pull (°C), t₂ = target mixed temperature (°C), and t₃ = temperature of the boiled mash (90 °C or more works well).
Worked example 3 — 130 hL of mash at 50 °C, target 64 °C
V = 130 × (64 − 50) ÷ (90 − 50) = 45.5 hL of mash to boil
On the brewhouse floor there is a shortcut: compute the pull from the water volumes of the mash kettle and cereal cooker instead of full mash volumes, adding a volume coefficient for the grist — a smaller coefficient (≈130) for thinner mashes at water-to-grist ratios above 1 : 3, a larger one (≈250) for thicker grists. In a two-decoction schedule for 1800 kg malt + 600 kg rice (46 hL + 34 hL of water, 12 °P target), the first pull lifts the mash to 68 °C, and the second pull of about 33 hL brings the mixed mash to the 78 °C filtration temperature.
What is raw-material utilization — and how do you measure brewhouse yield honestly?
Brewhouse (mash) yield is the percentage of the grist that ends up dissolved in the wort — the single most important yardstick of mashing work:
Because the 0.96 correction factor never changes and wort density tracks its concentration, every wort strength has a fixed brewhouse-yield coefficient (concentration × density × 0.96). Look up the coefficient for your wort — e.g. 11.4 °P → 11.42 — and the formula collapses to:
Grist mass comes from automatic weighing — recorded in the mashing computer or the batch report.
The 0.96 factor: hot wort is measured at ~100 °C but analyzed at 20 °C. Cool 26.4 hL of hot wort to 20 °C (assuming no evaporation) and it shrinks 4%, to 26.4 × 0.96 = 25.4 hL — and re-expands again when reheated.
Measurement reality: the 4% figure is not exact — hot wort also expands ~0.2%, and hop products shift it: whole hops add ~0.2% to hot-wort volume, pellet products much less. Modern brewhouses therefore use in-line flow meters or a calibrated measuring vessel (accurate to ±0.05%), which hop additions do not disturb.
Worked example — a Pilsner brew, two ways
Cast wort (with hot break) 331 hL; hops removed 3.31 hL of hot-wort volume; wort 10.7%, density 1.0411; grist 4600 kg.
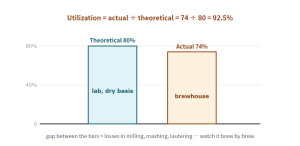
What matters far more is comparing the actual yield against the theoretical yield of the same malt. Theoretical yield comes from a standard laboratory mash of the raw material, reported as an anhydrous (dry-basis) extract. It depends on malt variety, modification and mill setting — generally 79–82% for pale malt and 75–78% for dark malt. Blend grists need a laboratory analysis of the actual mixture, taken at the right moment.
Table 1 — Theoretical (dry-basis) extract yields and the constants behind the formulas
Can one worked example tie the whole mash together?
The textbook closes the chapter with a full brewhouse calculation — grist, water, heat balance, mash thickness and sparging, all in one pass. Here is the complete chain:
Worked example 6 — 1000 L of 12 °P wort from malt + rice
Given: malt moisture 5%, rice moisture 13%; malt share 70%, rice 30%; dry-basis extract malt 80% / rice 95%; as-is extract malt 76% / rice 82.65%; first wort 17 °P; mashing-in at 48 °C, mash rest 65 °C, mash-out 100 °C; specific heats 1.6751 kJ/kg·°C (malt) and 1.8897 kJ/kg·°C (rice); 12 °P density 1.0484.
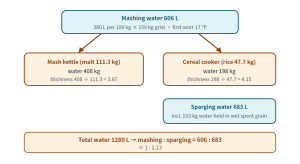
(7) Sparging water: with 120 kg of wet spent grain (80% moisture) per 100 kg of malt, the 159 kg grist leaves 191 kg of wet grain carrying 153 kg of water. Total water = 1136 + 153 = 1289 L → sparging = 1289 − 606 = 683 L, i.e. mashing : sparging = 606 : 683 ≈ 1 : 1.13
Table 2 — Worked example 6 at a glance
الخطوة
Result
Formula used
Mixed dry extract
84.5%
Weighted average (dry basis)
Mixed as-is extract
78%
Weighted average (as-is)
Total grist
159 kg (111.3 malt + 47.7 rice)
Grist formula with 0.96
Mashing water
380 L/100 kg → 606 L total
V = W(100 − Wp) ÷ Wp
Water split by heat balance
408 kg kettle / 198 kg cooker
Q = Cmt
Mash thickness
3.67 (kettle) · 4.15 (cooker)
water ÷ grist per vessel
Sparging water
683 L (ratio 1 : 1.13)
Total-water balance incl. wet grain moisture
Frequently asked questions about mashing calculations
1. What exactly does the 0.96 factor correct?
Wort contracts about 4% as it cools from 100 °C to 20 °C. Since extract is analyzed at 20 °C but volumes are measured hot, 0.96 converts the hot volume to the cold reference before any yield math.
2. Why does hot wort “show” 4% more volume than cold wort?
Thermal expansion. 26.4 hL of hot wort becomes 25.4 hL at 20 °C — and re-expands to 26.4 hL when reheated to 100 °C. Always compare volumes at the same reference temperature.
3. Do hops distort the measured brewhouse yield?
Whole hops add about 0.2% to hot-wort volume; pellet products add far less; hot-wort expansion contributes ~0.2% as well. Flow meters and calibrated vessels (±0.05%) remove almost all of this noise.
4. What first-wort concentration should I aim for?
It depends on your grist and beer style. For a 72%-extract malt, each °P of first wort trades against water: 16 °P needs 378 L/100 kg, 20 °P only 288 L. Choose the °P first, then let the formula set the water.
5. How large should a decoction pull be?
Typically one quarter to one third of the total mash. For the exact volume, use V = V₁(t₂ − t₁)/(t₃ − t₁); a 130 hL mash at 50 °C lifted to 64 °C with 90 °C boiled mash needs 45.5 hL.
6. What is a good raw-material utilization?
In the textbook example, 74% actual against an 80% theoretical extract gives 92.5% utilization. Compare only like with like — same malt, same laboratory method — otherwise the number means little.
7. Where does the “theoretical yield” come from?
From a standard laboratory mash of the raw material, reported as anhydrous extract: generally 79–82% for pale malt, 75–78% for dark malt. Blended grists need a lab analysis of the actual mixture.
8. Why does a 17 °P first wort become 12 °P cast wort?
Sparging rinses the remaining extract with hot water, diluting the first wort to the cast gravity. The water balance — 606 L mashing vs. 683 L sparging in worked example 6 — is what fixes the final 12 °P.
Want a brewhouse whose numbers line up brew after brew?
ZR Brewing builds two-vessel and four-vessel brewhouses with calibrated rousers, decoction-ready mash and cereal cookers, and accurate volume measurement — so the calculations above turn into repeatable, verifiable results.


 نُشر