

お見積りをご依頼ください
24時間以内にご返信いたします。お急ぎの場合は、WhatsAppまたはWeChat(+8613188932181)までご連絡ください。.
*当社はお客様のプライバシーを尊重し、すべての情報を保護いたします。.
お客様の情報は、お問い合わせへの回答にのみ使用し、未承諾のメールや宣伝メッセージを送信することは一切ありません。.
 公開日
Lautering process flow, first wort vs. sparging, technical targets, the four separation methods, and every factor that controls filtration speed.
Mashing is finished — the enzymes have done their job. But what happens next? The mash now contains dissolved soluble extract mixed with insoluble husks, proteins, and particles, and your beer will only be as clear, stable, and full-flavored as the wort separation that follows. Get lautering right, and you win twice: brilliant, well-tasting wort AND a high extract yield. Get it wrong, and you pay with slow cycles, hazy beer, and extract left behind in the spent grains. In this guide, we walk through the complete lautering process flow, the technical targets professionals measure, the four separation methods, and — most importantly — every factor that speeds up or slows down your run-off.
Once saccharification is complete, the breakdown of high-molecular substances in malt and adjuncts is done. The goal now? To separate the dissolved, soluble substances from the insoluble ones as quickly as possible — yielding a clear wort and a high extract yield at the same time. Sounds simple, but how is it actually done?
Wort separation splits into two distinct stages:
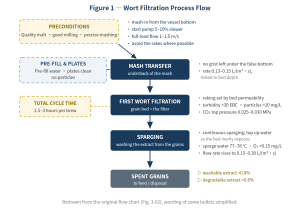
Notice the preconditions at the top: quality malt, a good mill gap setting, and precise mashing are decided before lautering even begins. Then three practical rules matter during mash transfer: pump the mash in from the vessel bottom, start the pump 5–10% slower than full load, and ramp up to the full-load flow of 1–1.5 m/s. Why so careful? Because a violent transfer disturbs the grain bed before it has even settled — and keep the false bottom free of grist particles underneath, or half your filtration area is wasted from the start.
The basic requirement sounds modest: separate the soluble extract from the mash quickly and completely. But here is the part many brewers underestimate — lautering is also a quality gate. You want to keep out of the wort everything that harms beer flavor and stability:
Keep these out, and you are rewarded with a wort that tastes clean and scores high on clarity. Let them through, and no amount of downstream processing fully repairs the damage.
How do professionals judge a lautering operation? By three groups of targets: wort quality, productivity, and environmental performance. The filtered wort must meet the quality the production plan demands, extract yield must be as high as possible, and the whole operation should minimize pollution. Here is the full scorecard:
| Category | Target | Ideal Value | Related Factors |
|---|---|---|---|
| Quality | Wort clarity (turbidity) | ≤30 EBC; short-term ≤10 EBC (wheat-beer wort slightly higher) | Fatty acids, flavor stability, bitter substances |
| Solids in wort | ≤30 mg/L, optimum is 0 | Fatty acids, flavor stability, iodine value, bitter substances, amount of trub returned to the whirlpool | |
| Iodine value | ≤0.25 ΔE; ≤0.3 ΔE after boiling | Filtrability, biological activity | |
| Oxygen content | <0.05 mg/L | Color, tannins, bitter substances, taste, flavor stability | |
| Productivity | High yield | Extract loss with the last wort ≤1%; lauter tun yield no more than 0.5% below the laboratory value | Malt cost |
| High speed (lauter tun) | 8–14 brews per day | Personnel, financing, investment | |
| Environmental | No residual sparge water | — | Ancillary equipment, staffing, quality, wastewater, cost |
| Grains-out step | Spent-grain residue on plates ≤400 g/m² | Small lauter tuns are hard to empty; wastewater | |
| Spent-grain pressing | Pressed juice handled in a closed system | Wastewater, odor | |
| Spent-grain disposal | Animal feed | Cost, landfill | |
| Underplate rinsing | Rinse water reused in the next brew | Wastewater, cost |
Source: Table 3-31. Two cells in the source photo were partially legible and are reproduced as printed where possible.
In commercial brewing, wort separation falls into four families. Which one fits your brewery?
Most large and medium breweries run methods (1) or (2), because they combine proven technology with gentle treatment of the grain bed. Small craft breweries increasingly consider the mash filter for its speed — but it demands finer milling and closer process control.
Why does one lauter run take 90 minutes and another three hours? The flow of wort through the grain bed is influenced by a whole chain of factors — and they should be considered from three angles. The process-side factors and their filtration effects are summarized below:
| Process Factor | Effect on Filtration |
|---|---|
| Malt quality | Degree of grist fineness (how well the husk stays intact) |
| Type and concentration of the mash | Viscosity of the mash |
| Type and concentration of adjuncts | Husk content and bed structure of the grain bed |
| Type and concentration of added enzymes | Viscosity of the mash (e.g., β-glucan breakdown) |
| Mashing method | Permeability of the grain bed |
| Mash transfer and temperature | Boundary layer forming on the false bottom plates |
| Mash transfer and pumping intensity | Shear force acting on the bed |
| Wort filtration process | Unit load (kg dry grist) on the false bottom |
Source: Table 3-32. The right-hand column of the source photo is partially legible; individual entries have been reconstructed to match standard lautering theory.
For a given lauter tun throughput, each of the following factors either accelerates or retards filtration when it increases. Can you predict which side each factor falls on?
| Accelerates Filtration (when increased) | Retards Filtration (when increased) |
|---|---|
| Looseness / permeability of the grain bed | Swelling of the spent grain (β-glucan hydration) |
| Open area of the false-bottom slots | Compressibility of the spent grain |
| Uniformity of the grain bed (no dense channels) | Thickness of the grain bed |
| Gentle, well-timed raking | Fines clogging the plate slots and bed pores |
| Filtering area actually in use | Excessive pressure differential across the bed |
Source: Table 3-33. The source photo is blurred and rotated; entries have been reconstructed from the legible headings and standard lautering theory.
The pattern is worth internalizing: everything that keeps the bed open, even, and incompressible helps you; everything that lets the bed swell, compress, or clog slows you down. Note the counterintuitive one — more pressure differential does not mean faster filtration. Push too hard and you compress the bed until it seals itself. That is why the CO₂ top pressure is capped at just 0.025–0.030 MPa.
Sparging looks like the simple stage — spray hot water, collect wort. But what separates a clean second wort from a disappointing one? Four details:
And when do you stop sparging? The stop point is defined by extract economics: stop when the washable extract remaining in the grains drops below 0.8% and the degradable extract below 0.8%. Pushing beyond that point waters down your wort for extract you barely recover — and the whole cycle is capped at 2.5–3 hours anyway.
Every brewer meets the stuck mash eventually. Run through this checklist before blaming the equipment:
First wort is drawn off while the full-strength mash flows through the fresh grain bed — it carries the highest gravity and the best flavor profile. Sparge wort (second wort) is what you rinse out of the grains with 77–78 °C water afterwards. Blending ratio decides your final gravity, which is why the ≤1% extract-loss target matters so much.
Above this range you start extracting husk tannins, pigments, and silicic acid, and residual starch can gelatinize into the wort. Below it, viscosity stays high and the rinse is inefficient. 77–78 °C is the compromise point.
Keep it gentle: 0.025–0.030 MPa. Higher differential pressure compresses the bed, seals the pores, and actually slows filtration — while also driving fines through the plates.
Target ≤30 EBC turbidity overall and ≤10 EBC in the short term, with solids under 30 mg/L — ideally zero. Wheat-beer wort runs slightly higher. If clarity drifts, check first wort return: recirculate the cloudy early runoff until it runs bright.
First wort filtration plus sparging should complete within 2.5–3 hours total, supporting 8–14 brews per day on a well-run lauter tun. If you regularly exceed that, revisit milling, bed depth, and your pressure profile.
Lautering is where your mash either becomes beer or becomes compromise. The process splits cleanly into first wort filtration and sparging, but success is decided earlier — at the mill, in the mash, and in how gently you transfer and treat the bed. Keep the quality targets (clarity, solids, oxygen), the productivity targets (yield, cycle time), and the environmental targets in view, respect the 0.13–0.15 L/(m²·s) first-wort rate, and never confuse pressure with speed.
Want to go deeper? Read our guides on mash agitator design and mashing technical conditions — because the best lautering starts with the best-prepared grain bed.
24時間以内にご返信いたします。お急ぎの場合は、WhatsAppまたはWeChat(+8613188932181)までご連絡ください。.
*当社はお客様のプライバシーを尊重し、すべての情報を保護いたします。.
お客様の情報は、お問い合わせへの回答にのみ使用し、未承諾のメールや宣伝メッセージを送信することは一切ありません。.