Brewhouse Quality Control: Can You Really Guarantee the Same Beer, Batch After Batch?
Brewhouse Quality Control: Can You Really Guarantee the Same Beer, Batch After Batch?
Zveřejněno
By zeren
Two brews, same recipe, same equipment — yet one batch pours brilliant and the next throws haze, throws off flavours, or drags your yield down. Where did it go wrong? The uncomfortable truth: quality is not tested at the end of the brewhouse, it is controlled from the very first grain. So what does a modern mashing cellar actually have to get right — and which trouble spots quietly sabotage uniformity? Let’s walk through the quality goals, the classic weak points, and the control philosophy that separates world-class brewhouses from average ones.
The correct target sounds modest: beer quality that at least meets the national standard — reliably, every single brew. Chasing an ever-higher quality level sounds admirable, but it drives costs up disproportionately. A modern brewhouse therefore balances fourteen requirements at once:
Good flavour and good economy
Justified energy investment with real saving measures
The necessary safety and automation systems
A good, comfortable working environment
Few maintenance and upkeep costs
Reliable operation
Low environmental burden — water and wastewater without contamination risk
Well-maintained equipment with low shear forces
Stable quality
Low oxygen pickup, few gum-forming substances — thanks to lower heating-surface temperatures
High flexibility
Low thermal load
Complete, quickly retrievable records
And the most important precondition: operators who love their work
Which 13 requirements does the brewhouse itself have to meet?
Quality control starts with hardware. A textbook-compliant mashing cellar is designed, built and commissioned against these rules:
Designed and accepted according to the relevant national standards
Piping designed so mash and wort are transported gently
No cavitation: pump suction openings sit at least 0.5 m below the lowest liquid level
Frequency-controlled (VFD) drives on all pumps
Grist dosing at the bottom of the vessel
Minimal air pickup during filling and emptying
Hygienic pipework and fittings
Valves and pipe plates that satisfy HACCP requirements
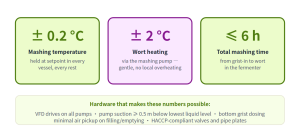
Mashing temperature controlled to within ± 0.2 °C of setpoint
Wort heating via the mashing pump controlled to within ± 2 °C
Lauter operation judged not only by differential pressure but also by wort flow
Total mashing time — grist-in to wort in the fermenter — must never exceed 6 h
Plus: records kept so any batch can be traced in minutes
How do you guarantee uniform quality — brew after brew?
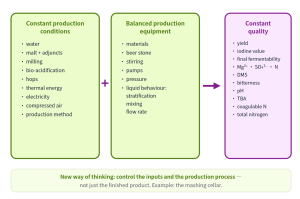
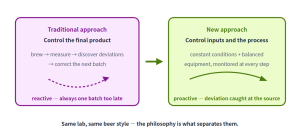
Uniformity is not an accident. The textbook’s schematic is brutally simple: inputs (necessarily intermittent) → production control → uniformity and quality. In practice that means two pillars stand side by side, and only their combination produces the third box — constant quality.
Look at what sits in the middle column: beer stone and liquid behaviour — stratification, mixing, flow rate — are equipment properties, not recipe choices. A brewhouse that layers, channels or scours unevenly will drift batch to batch no matter how disciplined the recipe is. That is exactly why vessel geometry, agitator design and pump selection belong in any serious quality conversation.
Which trouble spots lurk in every brewhouse?
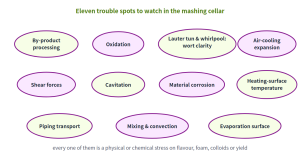
Before you can control quality, you need to know where it leaks. The textbook maps eleven physical and chemical danger zones in the mashing cellar — from by-product handling to the evaporation surface. How many of these does your brewhouse actively manage?
What holds traditional brewhouses back?
The textbook lists 16 weaknesses of the traditional mashing cellar. Read them as a checklist and you will notice they cluster into four families — milling & oxygen, mechanical stress, thermal load, and process-control gaps:
Table 1 — The 16 classic weaknesses of a traditional mashing cellar, grouped by family
Family
Weaknesses
Typical consequence
Milling & oxygen
Dry milling with poor classification · wet-milling transfer systems · milling that oxidises · oxidation of mash and wort · oxygen pickup during operation
Loss of reducing power, duller flavour, darker colour, fewer foam-positive proteins
Mechanical & hydraulic
Pump cavitation · uneven mixing · microbial contamination from dead zones in pipework
Shear damage, inconsistent conversion, wort acidification and butyric acid formation
Thermal load
Excessive heat load · heating surface too large · evaporation surface too large · reflux of kettle condensate · high thermal load in the whirlpool
Here is the leverage point: more than 40% of beer quality is determined by malt quality alone. Good malt shortens the process, saves energy and lifts almost every finished-beer parameter at once — see how tightly the operation column and the beer column of Table 2 mirror each other.
Table 2 — Advantages of good malt quality (after Table 3-59)
Operation
Finished beer
Shorter mashing process
Lighter colour
Lower energy consumption
Good foam
Shorter filtration time
Fewer fermentation by-products
Higher brewhouse yield
Good aroma
Promotes fermentation
Pure, full-bodied entry
Good filtration performance
Moderate bitterness
Better stability
Longer shelf life · better flavour stability
The buying lesson: every dollar saved on marginal malt is repaid with interest in longer boiling, more filtration downtime, hazier beer and shorter shelf life. Quality control in the brewhouse begins at the malt silo door.
Which key issues dominate the mashing process technically?
Strip the theory down and nine technical issues decide whether the mashing process protects or destroys quality. The recurring villains? Oxygen, mechanical action and heat — and the places they combine:
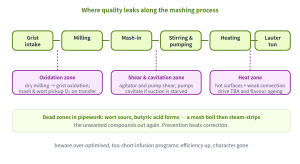
Oxidation from grist intake all the way to mash transfer
Mechanical action from stirring, pumping and careless pipework
Excessive convection and mixing of the mash — yes, beer stone can create beer off-flavours
High heating temperatures combined with poor convection (heating-surface temperature!)
Pump cavitation
Dead zones in pipework — where wort sours and butyric acid forms
The flip side: at mash boil, steam actually strips unwanted substances
Over-optimised, too-short infusion mashing — the danger of brewing a beer that tastes of nothing
Economically smart moves: reusing second sparge water, hot-water addition, or partial-mash methods to raise mashing-in temperature and enable acidification
What problems persist in real-world production?
Even well-equipped brewhouses struggle with human and process realities. The textbook names eight — do any of them sound familiar?
Teams cling to “the way we’ve always done it” and the auto-programs already set up — nobody wants to touch a running process
And for foam and α-amino nitrogen above all, mashing-in temperature is critical
So where should a brewer start tomorrow morning?
Verify the three numbers of Figure 1 on your own brewhouse: temperature ±0.2 °C, heating ±2 °C, total time ≤ 6 h
Walk the oxygen path from mill to lauter tun and seal every air-entry point — filling, emptying, transfer
Audit the pumps: VFD on every drive, suction openings ≥ 0.5 m submerged, no cavitation noise at full flow
Check your iodine value trend and α-amino N / zinc levels over the last 20 brews — drift is a process signal, not bad luck
Re-examine casting temperature if foam stability or FAN has slipped — it matters more than most brewers think
Frequently asked questions about brewhouse quality control
1. What is the correct quality target for a mashing cellar?
Beer quality that at least meets the national standard — consistently. Aiming far beyond that level raises costs disproportionately; uniformity and reliability create more value than occasional brilliance.
2. Why must mashing temperature hold ± 0.2 °C?
Enzyme systems respond steeply to temperature. A 1 °C drift shifts the beta/glucanase-to-amylase balance measurably, changing fermentability, FAN and filtration behaviour batch to batch.
3. Why is total mashing time capped at 6 hours?
Beyond roughly six hours from grist-in to wort in fermenter, microbial risk, oxidation load and dimethyl-sulfide precursor formation all climb, while foam-positive proteins degrade. Long brewhouse dwell time is a quality tax.
4. How can beer stone cause off-flavours?
Strong convection and mixing keep beer stone (calcium oxalate scale) particles suspended and scrubbing against wort; the textbook explicitly lists beer stone among equipment factors that create beer off-flavours. Clean vessels and gentle flow keep it bonded to the wall, not in your beer.
5. What is the TBA value and why track it?
The thiobarbituric-acid value indicates lipid oxidation load. High thermal load, oversized heating surfaces and large evaporation surfaces all push TBA up — and high TBA correlates with faster flavour ageing in the packaged beer.
6. Why does malt quality decide more than 40% of beer quality?
Malt supplies the extract, the enzyme potential, the nitrogen spectrum and most foam- and flavour-active precursors. Good malt simultaneously shortens mashing, cuts energy use, speeds filtration and lifts colour, foam, aroma and shelf life.
7. My wort zinc and FAN run low — what should I check first?
Check mashing-in temperature and grist dissolution first: both strongly influence FAN release, and casting temperature in particular is flagged as critical for foam and α-amino nitrogen. Then review whether trub separation is stripping too much zinc.
8. Is a shorter, “optimised” mashing process always better?
No. Over-optimised, too-short infusion programs may raise capacity but flatten beer character — the textbook warns they lead to bland beer that loses its typicity. Optimise towards a target flavour profile, not just towards minutes saved.
Want a brewhouse built for uniform quality from day one?
ZR Brewing engineers mashing systems around exactly these control principles: ±0.2 °C temperature control, VFD pump packages, bottom grist dosing, gentle pipework geometry and HACCP-compliant valves — so uniform quality is designed in, not hoped for.


 Zveřejněno