100L Multi-functional Distiller
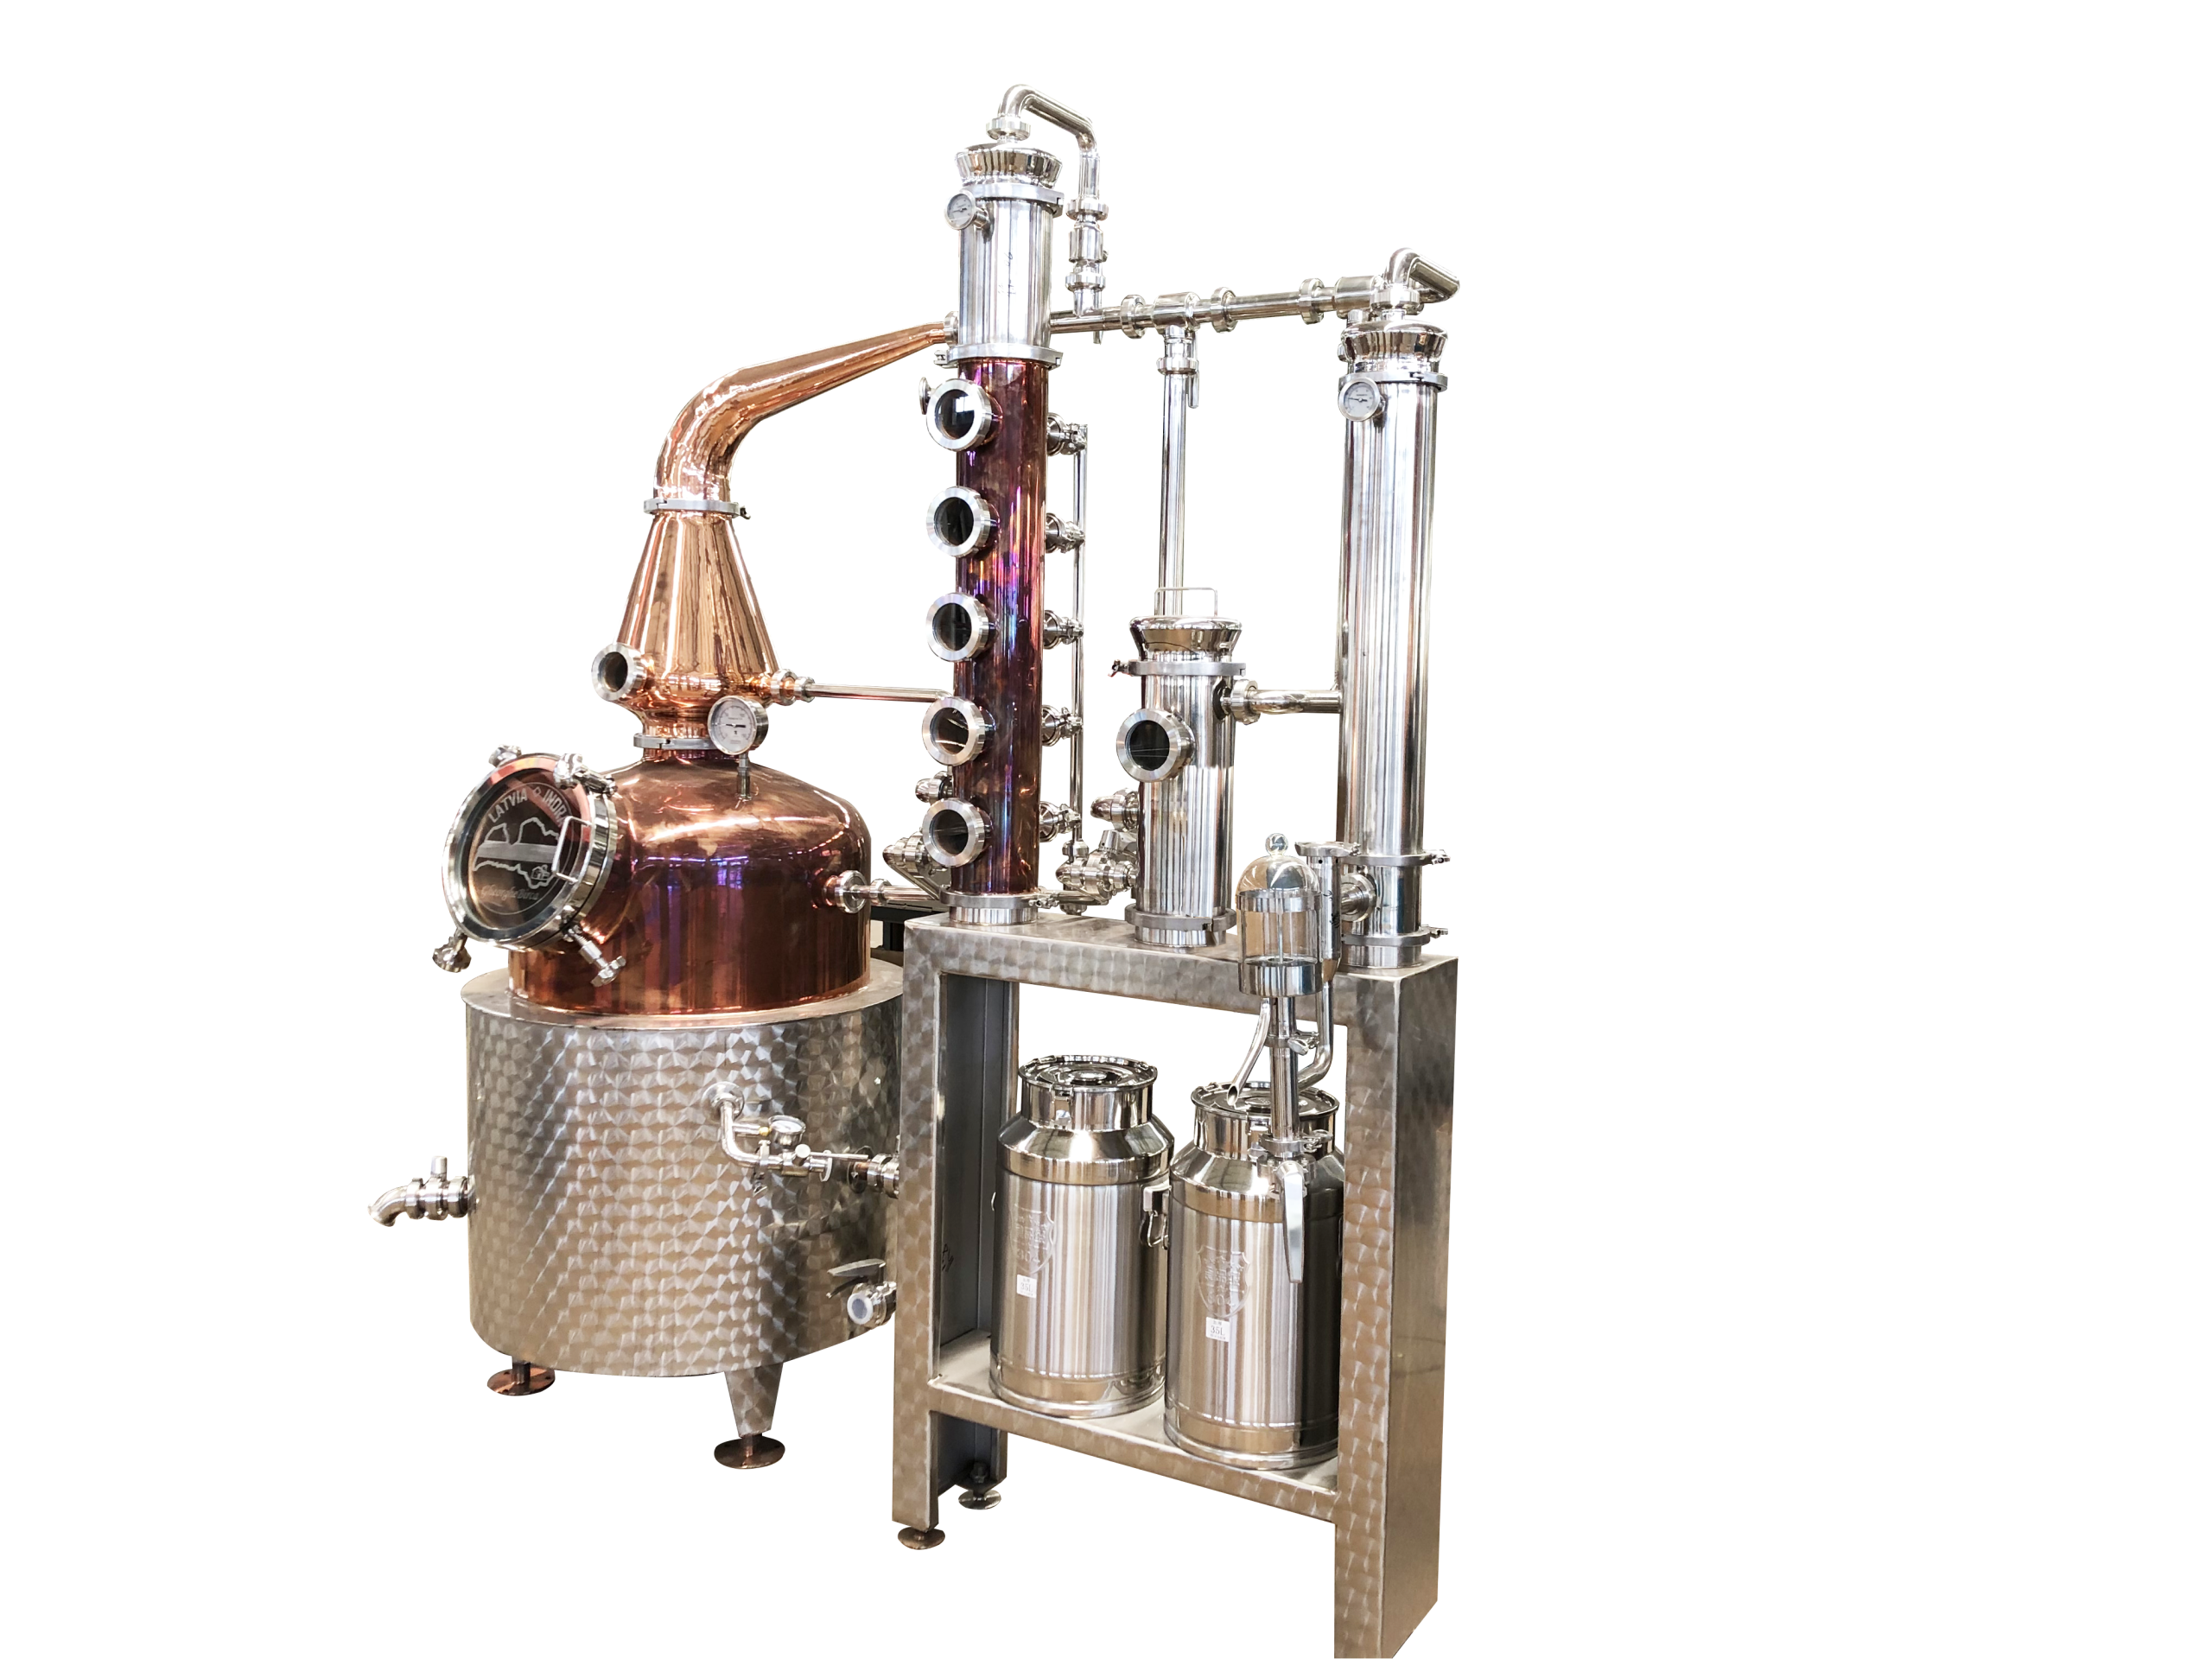
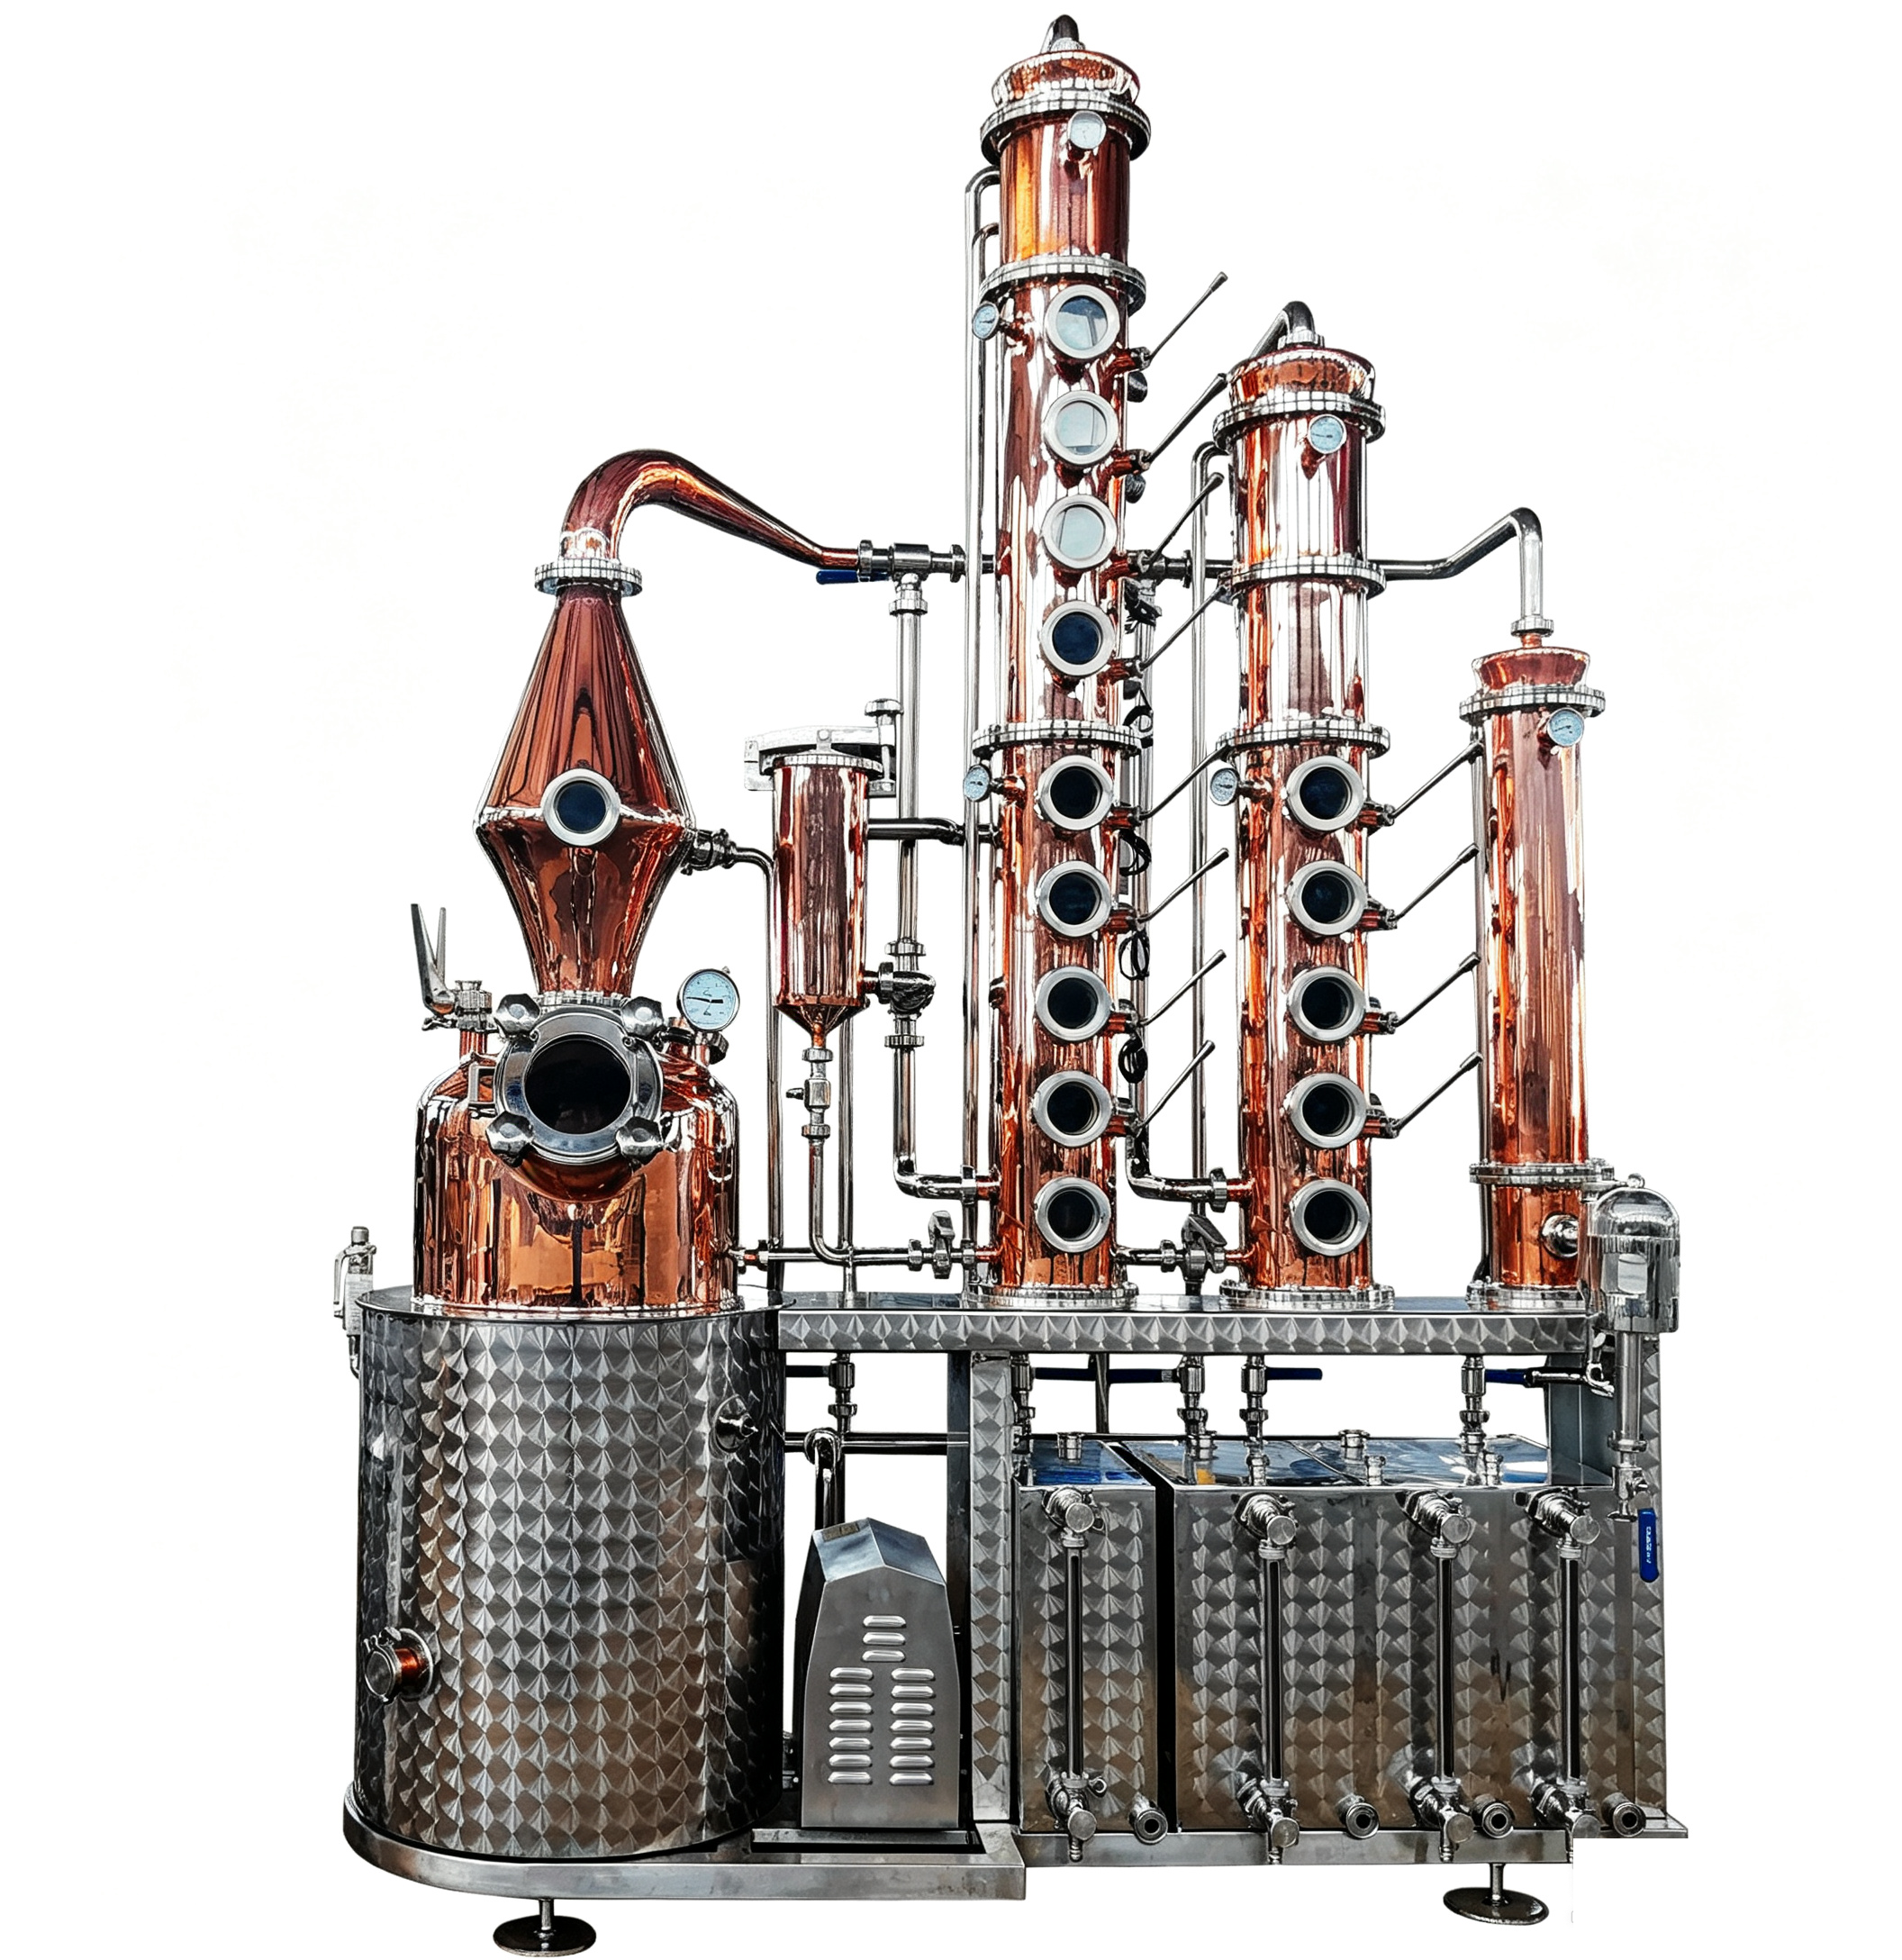
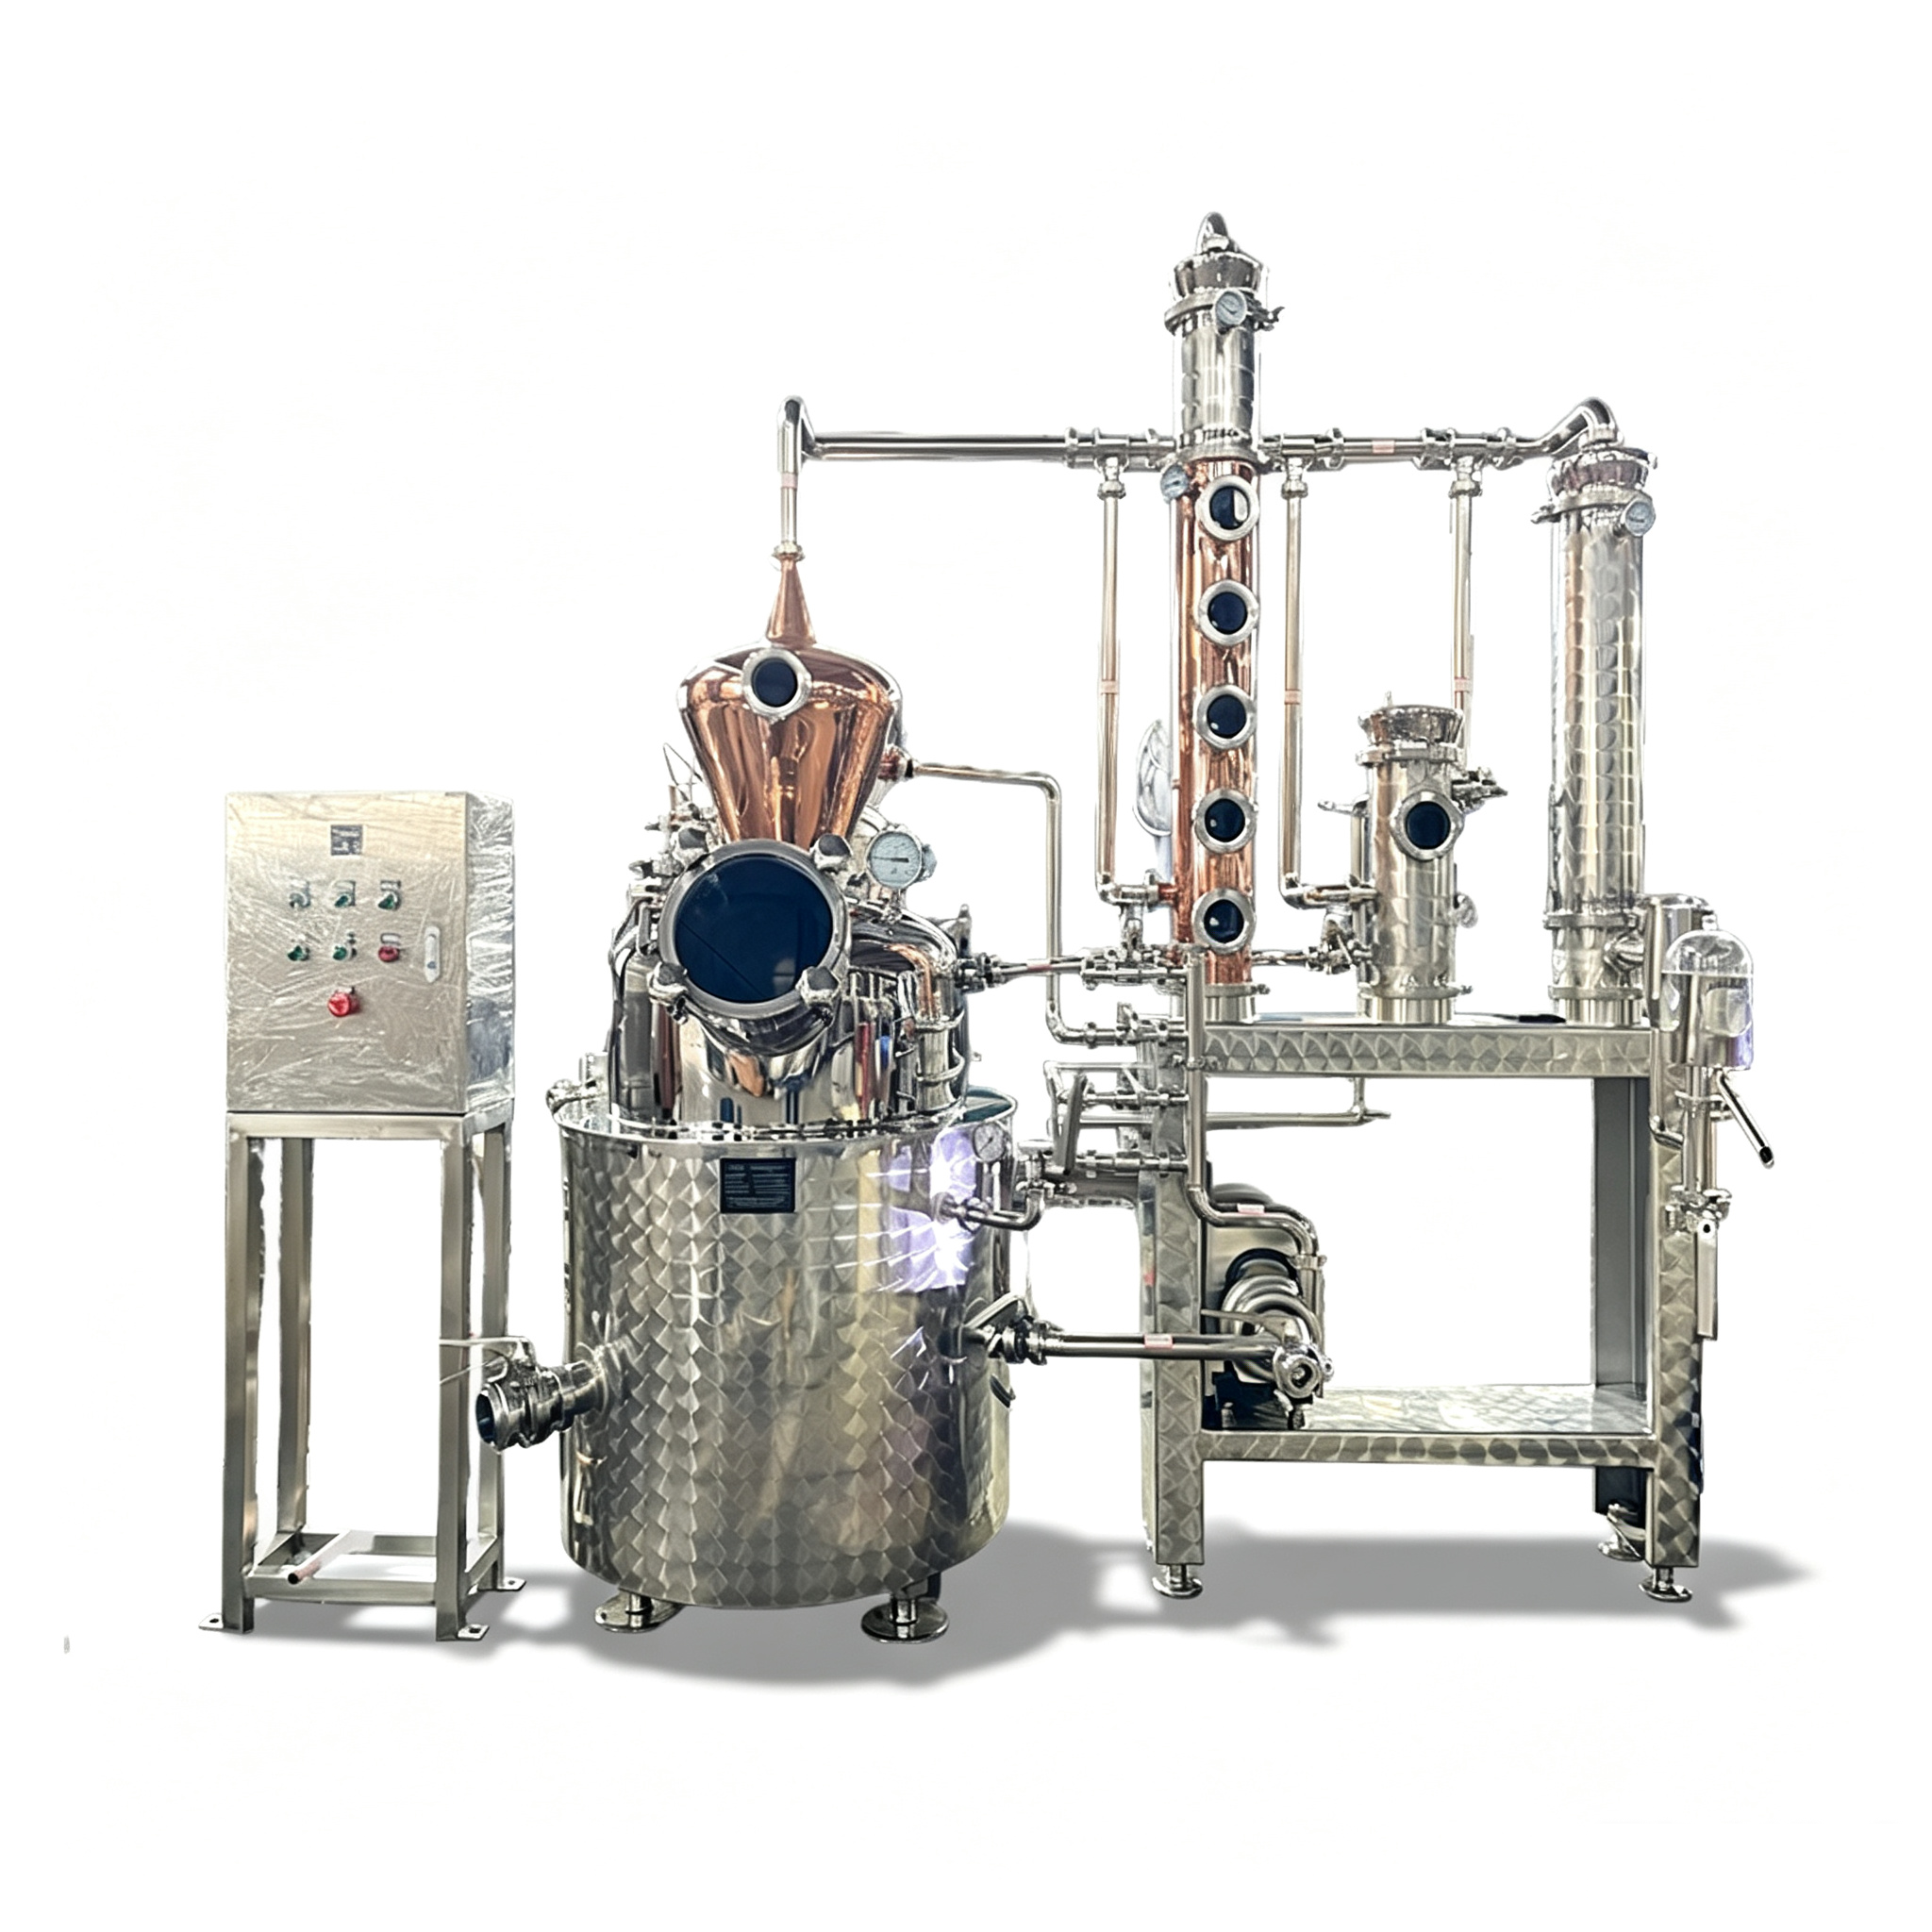
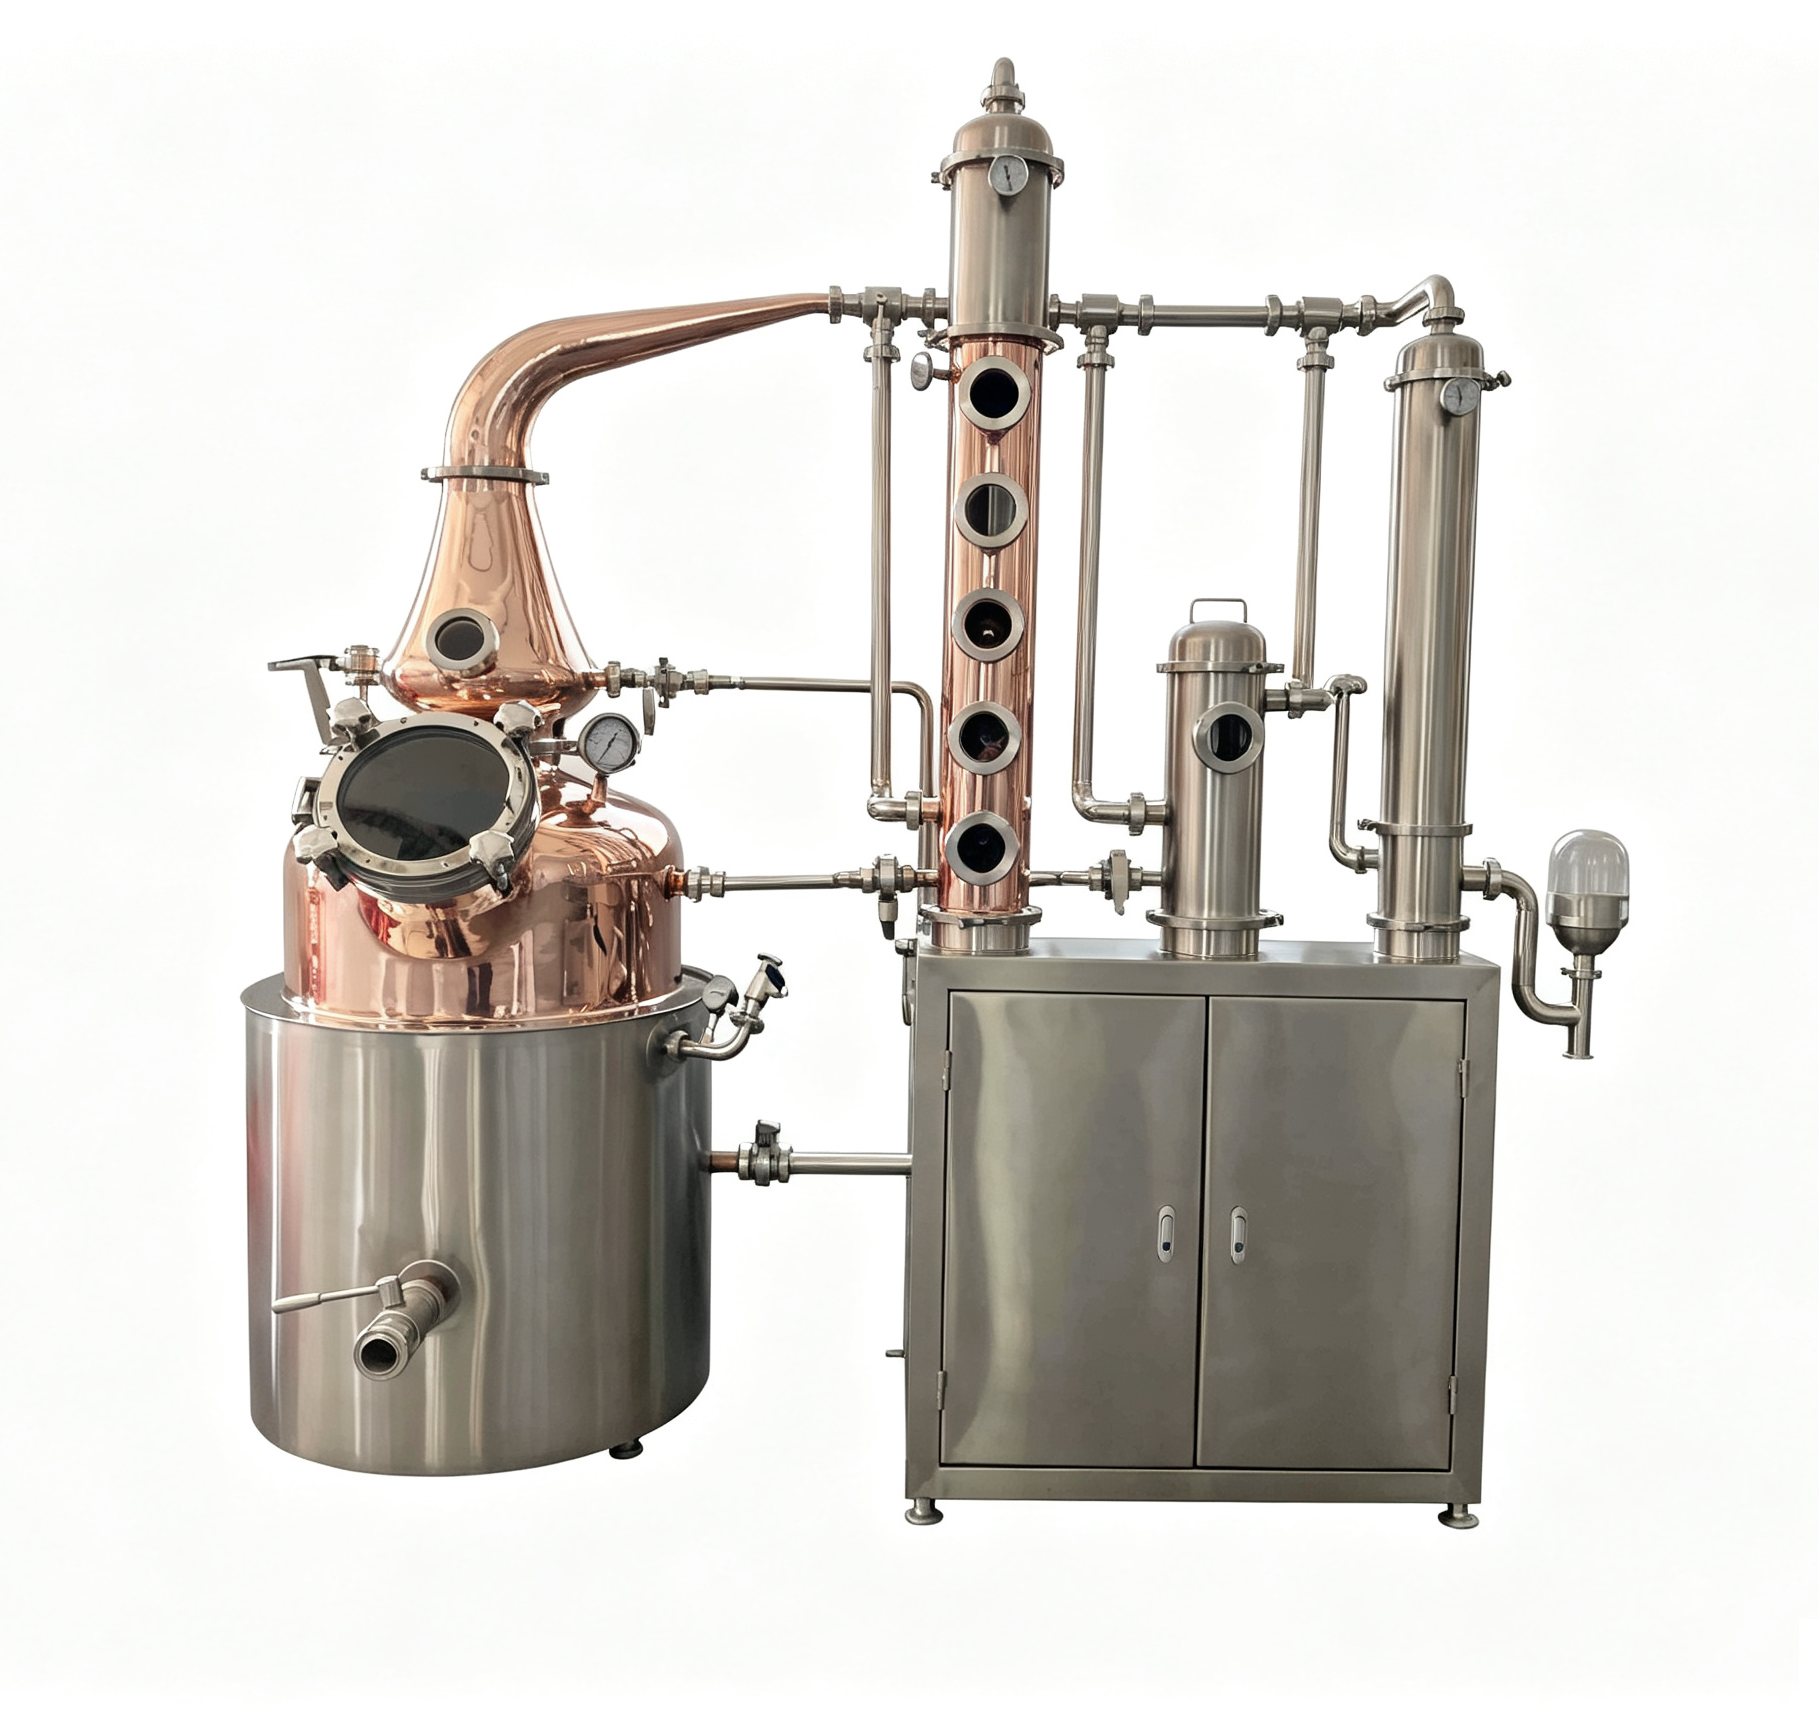
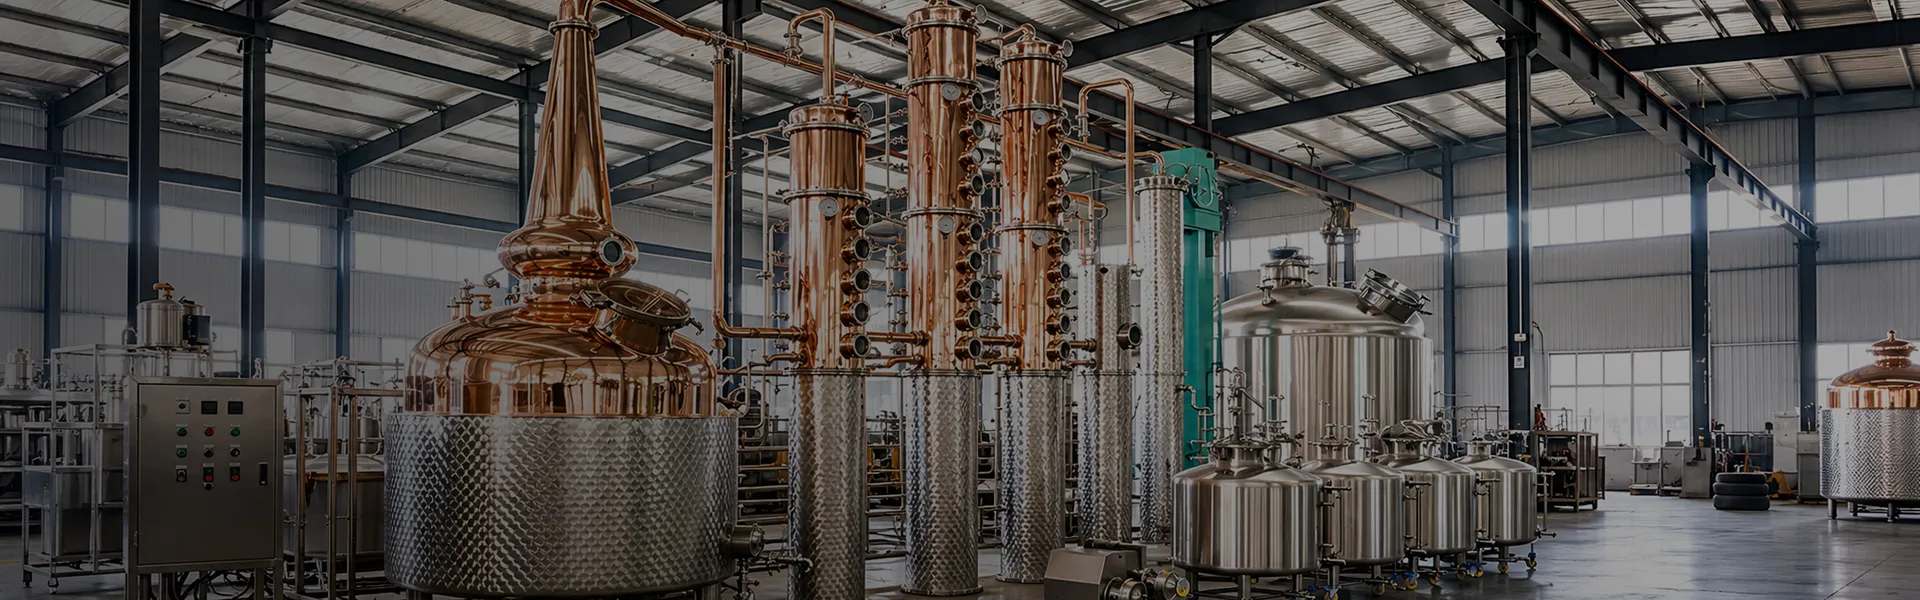
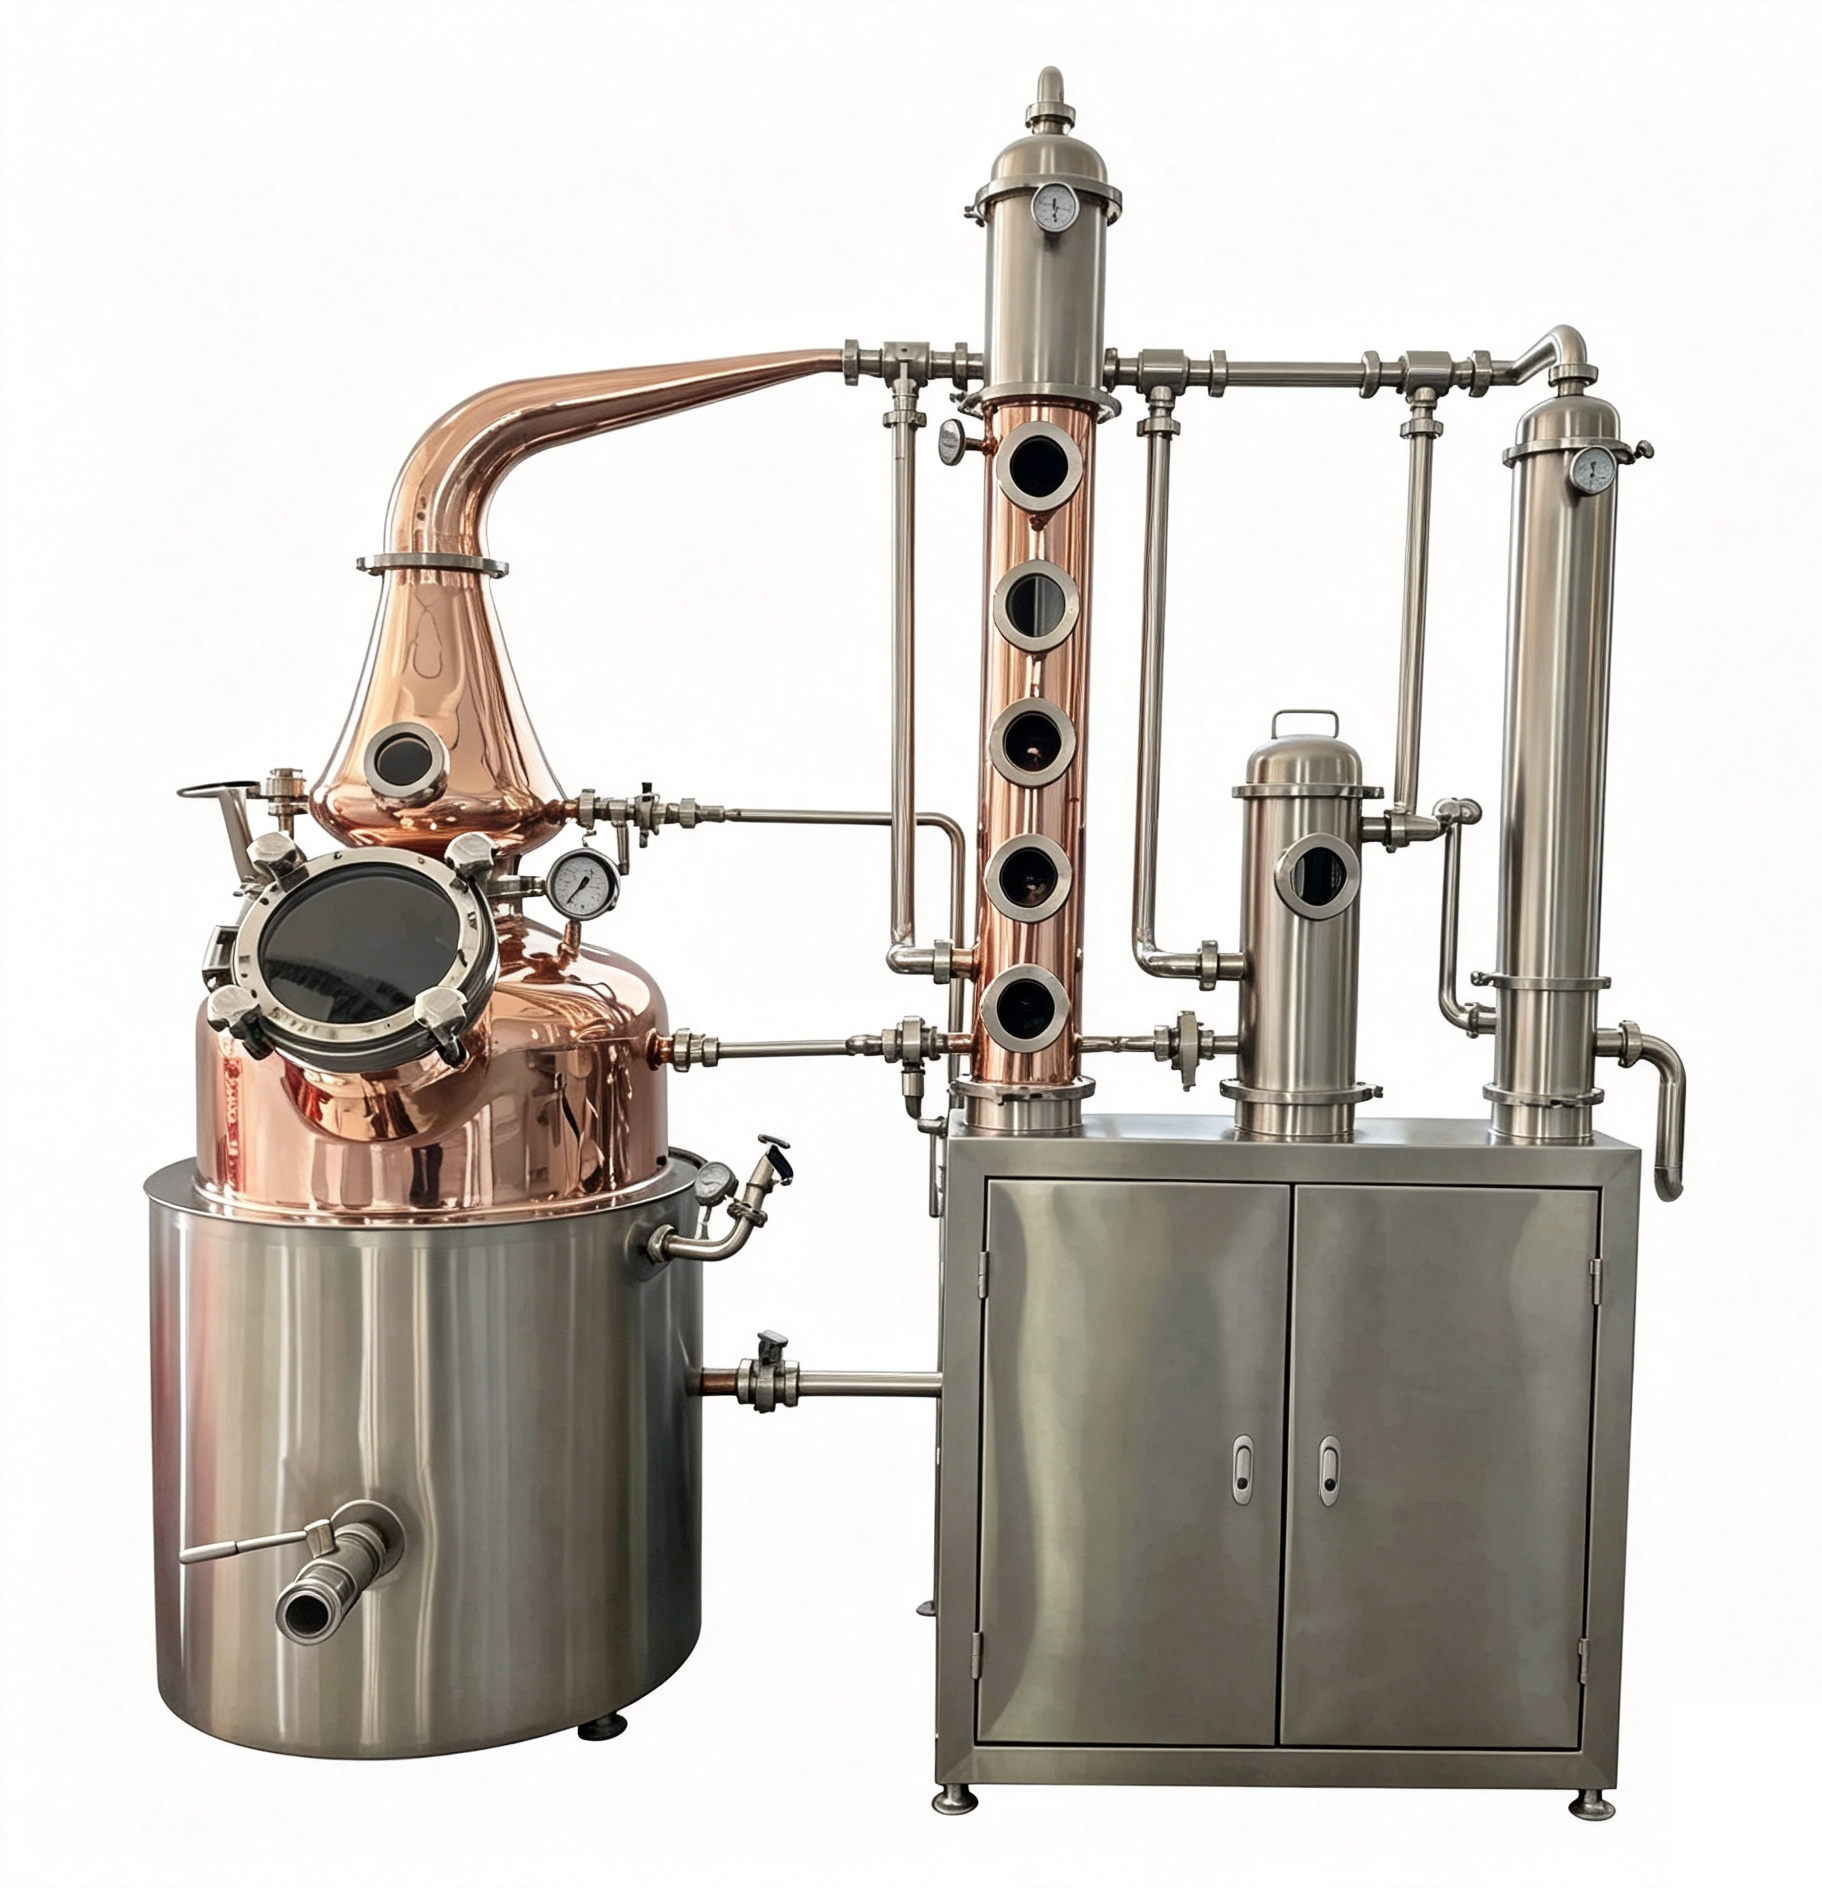
The 100L Multifunctional Distiller (Model: ZR-DT-100L) is a compact, versatile spirits distillation system designed for small commercial distilleries, craft spirits producers, and serious pilot-scale distilling operations. With an effective volume of 100 liters and a configurable still design featuring a 5-plate copper and stainless steel fractionating column, this unit supports the production of whiskey, brandy, rum, gin, and vodka within a single, adaptable system. The boiler is constructed with a red copper dome and neck for superior catalytic removal of sulfur compounds, paired with a food-grade 304 stainless steel jacket for durability and easy maintenance. Equipped with a large sight glass on the boiler, multiple observation ports along the column, precision pressure and temperature gauges, and dual condensers, the system offers full process visibility and control. Built from food-grade stainless steel and red copper based on buyer specification, it is particularly well-suited for craft distillery startups, brewpubs exploring spirits production, and investors establishing a small-scale distilling facility.
 Отправить запрос
Подробности